2026年10月28日星期三

Self Loading Mobile Concrete Mixer

 Self loading mobile concrete mixers combine loading, batching, mixing, travel, and discharge functions in one machine. That integration reduces dependence on separate equipment, but it also makes parts selection more demanding. A failed hydraulic hose, drum blade, axle seal, or sensor can stop concrete production and delay an entire pour.

For fleet owners and project managers, the practical objective is not to hold every component in stock. It is to identify high-risk wear items, verify fitment before ordering, and build a service plan around operating hours, material abrasiveness, and local parts lead times.
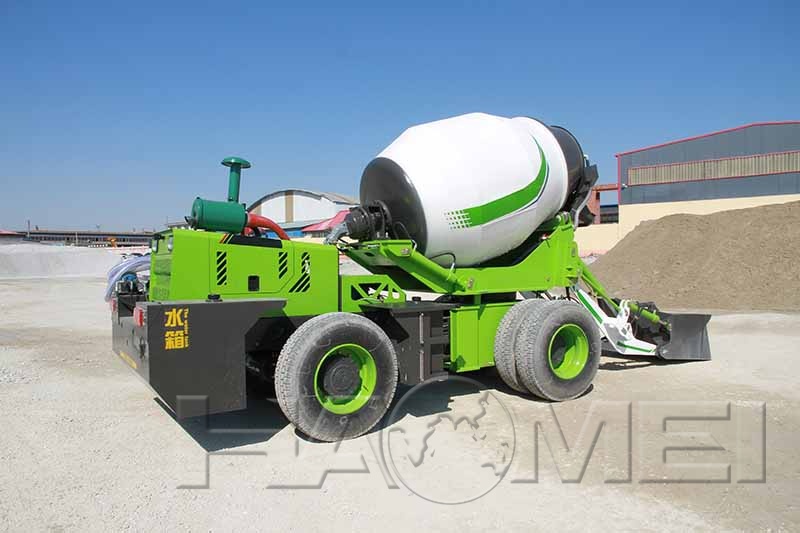
self loading concrete mixer machine

Identify the Parts That Cause the Most Downtime

Start with the machine's parts book, serial number, engine model, axle model, hydraulic-pump identification plate, and drum capacity. A mixer model name alone is not enough for accurate ordering. Manufacturers can change hose routing, sensor connectors, pump displacement, or brake assemblies during a production run.

Use this three-step check before approving a purchase order:

  1. Match the OEM part number against the serial-number range in the manual.
  2. Confirm dimensions and technical data, including thread type, voltage, pressure rating, tooth count, and seal material.
  3. Compare the failed part with the replacement before installation, especially for hydraulic, electrical, and brake components.

The following table helps prioritize stock based on typical operating exposure.

Part groupCommon failure mechanismStock recommendationVerification before fitting
Mixing blades and scrapersAbrasion from aggregate and cement slurryKeep a planned replacement set for high-hour machinesBlade profile, bolt pattern, drum direction
Hydraulic hoses and fittingsAbrasion, heat, contamination, hose agingStock common hose sizes and approved fittingsPressure rating, fitting series, hose length, routing
Hydraulic filtersContaminated oil and missed service intervalsKeep filters for every fleet modelFilter part number, bypass specification, seal size
Seals and cylinder kitsRod damage, heat, contaminated oilStock for heavily used cylindersCylinder bore, rod diameter, seal compound
Wheel bearings and hub sealsDust, water ingress, overloadKeep when machines travel frequently on rough sitesAxle model, hub dimensions, torque procedure
Electrical sensors and switchesVibration, moisture, connector damageKeep critical safety and batching sensorsConnector type, supply voltage, calibration requirement

Mixing components deserve special attention. Worn blades lower mixing efficiency and can leave hardened concrete in the drum. Replacement should be scheduled before a blade wears through or its mounting area becomes damaged. During planned blade work, inspect drum liners, mounting bolts, discharge chute pivots, and gearbox supports at the same time.
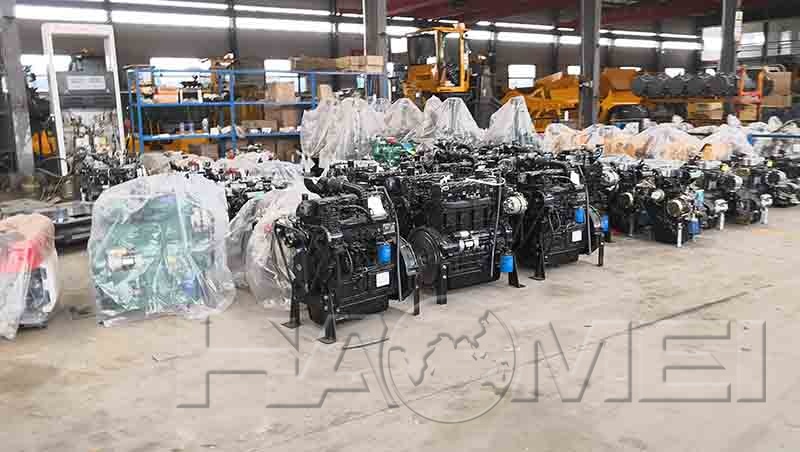
spare pars of self loading mixer

Choose OEM, Equivalent, or Rebuilt Components by Risk

Not every item requires the same sourcing strategy. Consumables such as correctly specified filters and standard fasteners may be available from reputable industrial suppliers. However, parts affecting steering, braking, hydraulics, load handling, or machine controls need stricter fitment and traceability controls.

Purchase optionAppropriate useMain benefitMain control needed
OEM partSafety-related, electronic, structural, drivetrain, and warranty-sensitive itemsKnown fitment and documented specificationConfirm current part-number supersession
Qualified equivalentFilters, hoses, bearings, seals, and standard electrical items when specifications matchCan reduce lead time and procurement costObtain technical datasheet and verify interchange data
Rebuilt componentSelected starters, alternators, hydraulic cylinders, and pumps from a qualified rebuilderMay reduce acquisition cost and material wasteRequire test record, warranty, and core-condition assessment

Do not select hydraulic hose only by outside diameter. The replacement must meet the required working pressure, temperature range, fluid compatibility, bend radius, and fitting type. ISO 4413, Hydraulic fluid power - General rules and safety requirements for systems and their components, is a recognized reference for hydraulic-system safety. It supports practices such as depressurizing systems before work, preventing hose abrasion, and controlling leakage hazards.

For braking, steering, and rollover-protection-related repairs, use the manufacturer's approved components and tightening procedure. Changes to machine safety systems can affect regulatory compliance and insurance coverage. In the United States, site operators should also assess applicable OSHA construction requirements, including the general equipment provisions in 29 CFR 1926 Subpart O. Requirements vary by jurisdiction and machine classification.

A practical investment comparison is to calculate downtime exposure rather than focus only on invoice price. Record these values for each critical part:

  • Average delivery lead time.
  • Labor hours to replace the part.
  • Lost production hours if the machine stops.
  • Cost of delayed concrete placement, standby labor, and hired replacement equipment.
  • Failure frequency from service records.

A low-cost seal kit may justify shelf stock if its absence stops the mixer for several days. A costly electronic controller may be better supplied through a rapid-delivery agreement unless the fleet operates many identical units.

For capacity planning, compare specifications and service commonality across a HM3.5 Self Mixer and a HM4.0 Self Mixer. Standardizing a fleet around fewer models can simplify filters, hoses, sensors, training, and diagnostic tools.

Build a Parts and Maintenance System That Prevents Emergency Orders

Create a machine-specific register rather than a generic inventory list. Each record should include the asset number, serial number, component supplier, approved alternatives, last replacement date, running hours, storage location, and supplier lead time.

Use the following inspection rhythm, then adjust it to the manufacturer's maintenance schedule and site conditions.

IntervalInspection actionsParts decision
Daily before operationCheck fluid leaks, hose rubbing, tire condition, blade bolts, chute pivots, lights, alarms, and visible wiringTag damage and stage urgent replacements
WeeklyInspect filter indicators, hydraulic fittings, battery terminals, drum drive area, grease points, and wheel-end leakageOrder items showing early wear
At scheduled service hoursReplace fluids and filters as specified, inspect oil samples where used, check brake and steering componentsReplenish consumed stock and update failure history
Before major poursConfirm spare hose, filter, electrical fuse, seal kit, and emergency repair tools are availableProtect the production schedule from common stoppages

Store rubber seals, hoses, and electrical items away from direct sunlight, ozone sources, moisture, and excessive heat. Keep hydraulic fittings capped until installation. Contamination introduced during a rushed repair can damage pumps, motors, and valves that cost far more than the original failed item.
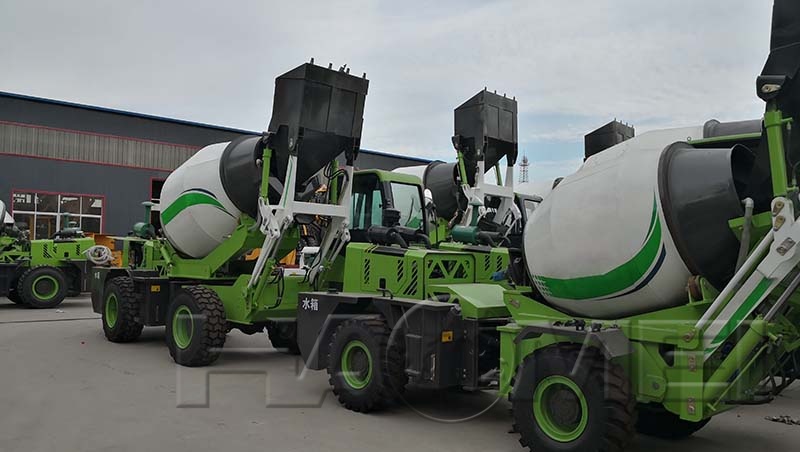
self loading mixer factory

Digital maintenance records are increasingly useful for mobile mixers. Hour-meter data, fault codes, oil-analysis reports, and work orders can reveal repeat failures by machine, site, operator shift, or component batch. If a hose repeatedly fails at one location, correct the clamp position or protective sleeving rather than repeatedly replacing the hose.

When requesting a quotation, provide a clear technical package: machine serial number, photographs of identification plates, part number, quantity, operating environment, required delivery date, and whether the machine remains under warranty. Ask the supplier to state warranty terms, country of origin where relevant, included seals or hardware, and any installation or calibration requirements. This documentation reduces incorrect deliveries and supports disciplined lifecycle-cost control.

Original Source: https://www.self-loading-mixer.com/a/self-loading-mobile-concrete-mixer-spare-parts.html

39m Concrete Pump: 5 Questions on Reach, Output, Cost

 A 39m concrete pump is often considered by contractors moving from line pumping to a truck-mounted boom pump, or replacing an older mid-range unit. Recent discussions across equipment forums, Google searches, and construction Q&A communities commonly focus on whether a 39m boom offers enough reach, what output is realistic on site, and which operating details affect long-term ownership.

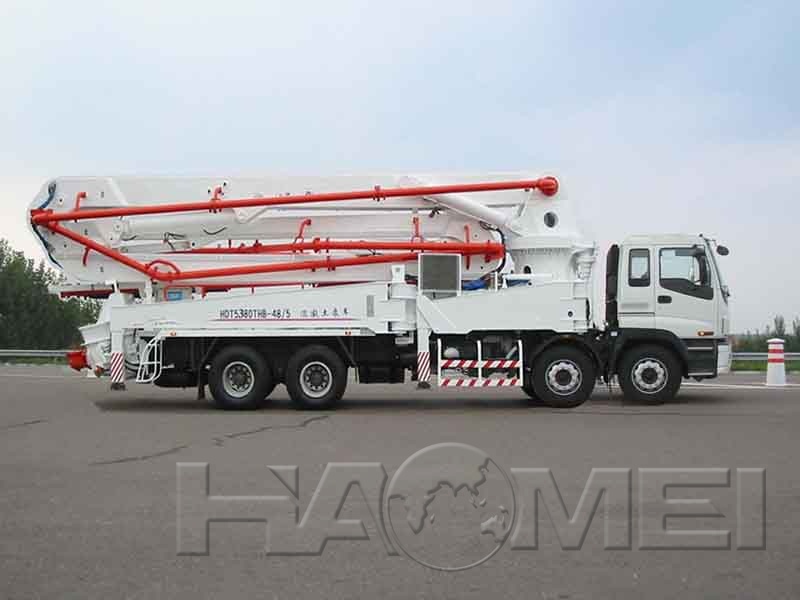
concrete boom pump truck

1. Is a 39m concrete pump large enough for most residential and commercial work?

For many low-rise and mid-rise projects, a 39m concrete pump offers a practical balance between reach, mobility, and setup requirements. It is commonly suitable for villa foundations, housing developments, warehouse slabs, retaining walls, bridge approaches, and commercial buildings where the placing point is within a moderate distance of the truck.

The stated 39m figure refers to boom length, not guaranteed horizontal reach at every angle. Actual working reach changes with boom articulation, truck position, elevation difference, and whether the boom must work around obstructions. A boom that can reach a distant slab edge in an open area may have less usable reach when it must pass over a wall, trees, utility lines, or an existing structure.

Before selecting a machine, request the manufacturer's boom placement diagram. It should show vertical reach, horizontal reach, depth reach, and the dimensions of the boom's unfolding envelope. A 39m class unit is usually more versatile than a 37m machine where job sites have limited truck access but still require placement across wider foundations or elevated floor slabs.

For projects needing a balance of maneuverability and reach, a HDT5291THB-37/39/4 Concrete Pump Truck is relevant because it places the 37m and 39m boom options in a similar operating category.

2. What concrete output can a 39m concrete pump deliver per hour?

A 39m concrete pump's theoretical output is often listed around 100 to 160 m3/h, depending on the pumping system, cylinder diameter, stroke length, engine power, and hydraulic configuration. On a real pour, delivered output is usually lower than the catalog maximum.

Typical site output may range from 50 to 100 m3/h when batching, truck arrival timing, mix consistency, hose handling, and crew coordination are normal. High-volume slab pours can achieve stronger results when ready-mix trucks arrive continuously and the concrete has a pumpable, stable design. Conversely, output can fall sharply if trucks queue irregularly, the mix is too stiff, or the operator repeatedly relocates the boom.

FactorEffect on Actual Pumping Output
Ready-mix truck schedulingDelays create empty pumping cycles and reduce hourly volume.
Slump and mix designA cohesive pumpable mix flows more consistently through the pipeline.
Aggregate gradingPoor grading or oversized aggregate raises blockage risk.
Pipeline conditionWorn pipes, elbows, and couplings increase resistance.
Boom movement frequencyFrequent repositioning slows continuous placement.
Operator and placing crewExperienced coordination improves pour speed and finish quality.

Do not size a pump only by its maximum m3/h rating. Compare the hydraulic pressure, pumping-cylinder dimensions, allowable aggregate size, and expected pipeline length. For a long horizontal run, vertical rise, or demanding mix, pressure capability can matter as much as output volume.

concrete boom pump

3. How much space does a 39m concrete pump need for setup?

This is one of the most important questions because a boom pump that cannot deploy safely is of little value at the project site. A 39m concrete pump needs space not only for the truck chassis but also for its outriggers and boom unfolding path.

Outrigger width varies by model and may be several meters wider than the truck body. Some machines use X-style outriggers, while others use front swing-out or compact-outrigger designs intended for tighter urban locations. Ask for the exact dimensions for full extension, one-side extension if permitted, and the required ground bearing conditions.

The setup area must also be level and capable of carrying concentrated outrigger loads. Soft ground, recently backfilled trenches, drainage covers, basement slabs, and unsupported pavement can create serious stability hazards. Proper outrigger pads help spread load, but they do not compensate for ground that lacks adequate bearing capacity.

A pre-pour site check should confirm truck approach width, turning room, overhead power lines, boom clearance, mixer-truck access, and safe separation from excavation edges. The required space is determined by the entire pumping operation, not merely the vehicle's parked footprint.

4. Can a 39m concrete pump handle high-strength or low-slump concrete?

Yes, but the mix must be designed for pumping and the equipment must be matched to the application. High-strength concrete can be pumped successfully, yet a high cementitious content, low water-cement ratio, fibers, admixtures, and angular aggregate may increase line pressure and make flow less forgiving.

Low-slump concrete is not automatically unsuitable, but it needs careful testing. A mix that appears workable in the discharge chute may still be difficult to pump through a long pipeline or a fully extended boom. The pumping contractor should review slump flow, aggregate size, fines content, admixture timing, and air content before the pour begins.

For demanding concrete, use a compatible primer or grout, maintain a continuous supply, avoid unnecessary stoppages, and monitor pressure changes. Abrupt pressure increases can indicate segregation, a developing blockage, a closed valve, or a pipe issue. Pumping should stop and be assessed before excessive pressure damages components or creates unsafe conditions.

5. What operating costs should be considered beyond the purchase price?

A new 39m concrete pump involves expenses beyond the truck and boom system. Fuel consumption, chassis service, hydraulic oil, wear plates, cutting rings, delivery pipes, elbows, seals, remote-control maintenance, tires, inspections, and trained operators all influence the cost per cubic meter pumped.

Wear parts deserve special attention. Concrete abrasion affects the S-valve or rock valve area, hopper components, pipe bends, end hoses, and boom delivery line. Abrasive aggregates, high pressure, inadequate cleaning, and improper lubrication can shorten component life. A consistent washout and inspection routine is far less expensive than an unexpected breakdown during a scheduled pour.

Ownership AreaQuestions to Ask Before Selecting a 39m Pump
Pumping systemWhat are the rated pressure, output, cylinder size, and valve design?
Boom structureWhat is the boom section design and inspection schedule?
ChassisIs local service available for the engine, transmission, and suspension?
Parts supportAre pipes, seals, wear plates, and electronic parts readily stocked?
ControlsDoes the remote system provide diagnostics and reliable emergency functions?
Resale potentialIs the model configuration common in the intended operating market?

A Concrete Pump Truck with accessible service points, clear diagnostic functions, and locally obtainable wear parts can reduce downtime significantly. When comparing models, evaluate the complete support package, including commissioning, operator training, parts availability, warranty scope, and technical response time.

new concrete boom pump for sale

Original source: https://www.haomei-machinery.com/a/39m-concrete-pump.html

What Is Concrete Pump Truck Price

A concrete pump truck is a major investment for contractors handling foundations, high-rise structures, bridges, and large commercial pours. The final concrete pump truck price depends on far more than boom length. Chassis brand, pumping output, hydraulic configuration, control system, emission standard, material quality, and local service support all affect the total purchase cost and long-term operating value.

A lower initial quotation may be attractive, but equipment selection should focus on matching the machine to jobsite requirements. A truck with insufficient boom reach, limited output, or difficult service access can create higher costs through lost productivity, repair downtime, and additional labor.

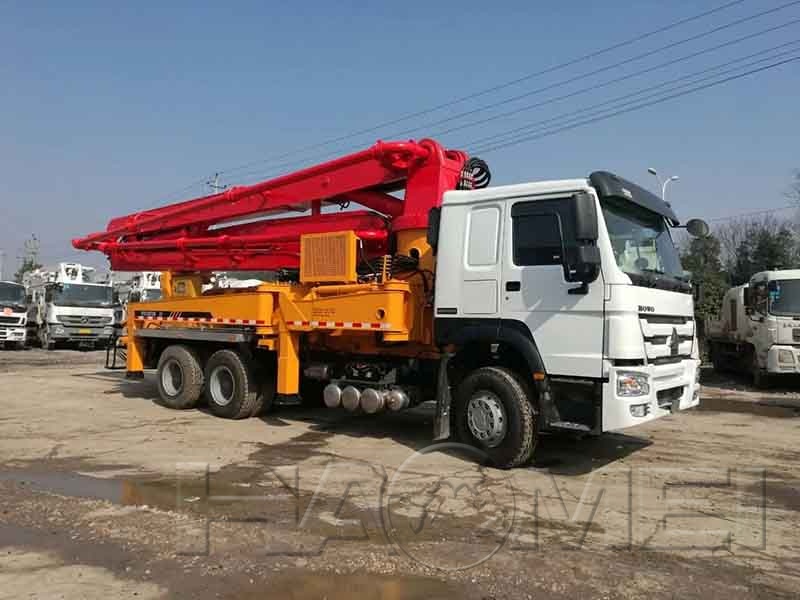
concrete boom pump truck

What Determines Concrete Pump Truck Price?

Boom length is one of the main cost drivers. Short-boom units, commonly used for low-rise housing and confined sites, generally require less structural steel and have lower chassis demands. Mid-range models are suitable for many commercial projects, while long-boom machines require stronger boom sections, more complex stabilization systems, and larger truck chassis.

For example, a 42m Concrete Pump Truck can provide a practical balance of reach, maneuverability, and pumping capacity for many urban construction projects. Larger units are better suited to wide foundations, tall structures, and sites where the truck must remain farther from the placing area.

Price FactorWhy It Affects CostWhat to Check
Boom length and configurationLonger booms need more steel, stronger joints, and higher stability capacity.Reach diagram, unfolding space, boom section design.
Pumping outputHigher output requires larger cylinders, valves, and hydraulic capacity.Theoretical output, pressure, cylinder diameter.
Chassis specificationA heavy-duty chassis supports boom weight and road transport loads.Engine power, axle layout, payload rating, local compliance.
Hydraulic systemEfficient hydraulic design affects fuel use, heat control, and response.Pump brand, cooling system, filtration, maintenance access.
Wear componentsHigh-quality wear parts reduce shutdowns in abrasive concrete service.Wear plate, cutting ring, delivery pipe, piston material.
Service availabilityFast parts supply and trained technicians reduce downtime.Local inventory, warranty terms, diagnostic support.

Transportation, import duty, registration, insurance, and commissioning may also affect the delivered equipment cost. Ask for a clearly itemized quotation that identifies the chassis, pump unit, boom configuration, included pipeline, remote control, spare parts, and warranty coverage.

Design and Material Features That Create Long-Term Value

Modern pump trucks combine a truck-mounted chassis, hydraulic pumping system, multi-section placing boom, hopper, delivery pipeline, and electronic controls. Each system must work together under high pressure and repeated load cycles.

The boom is typically fabricated from high-strength structural steel to improve strength while controlling overall weight. A lighter but properly engineered boom can improve stability, reduce chassis loading, and support smoother boom movement. Weld quality, stress-relief practice, boom pin design, and inspection procedures are important because the boom carries cyclic loads during every pour.

A Z-fold boom arrangement is widely used because it provides flexible placement around obstacles and can operate in relatively limited spaces. For projects that need greater horizontal reach, a 45 Meter Z Boom Concrete Pump may offer efficient coverage while retaining useful placement flexibility.

32 meter concrete pump

The pumping unit should use durable wear-resistant components in the concrete valve area. The wear plate and cutting ring are exposed to high-pressure, abrasive concrete flow. High-quality alloys and proper lubrication help extend service life. Chrome-plated concrete cylinders, robust pistons, and hardened delivery pipes also reduce wear when pumping mixes containing coarse aggregate.

Hydraulic design is equally important. A properly sized hydraulic oil cooler helps control operating temperature during continuous pumping. Clean hydraulic oil protects pumps, valves, and cylinders. Systems with accessible filters, readable gauges, and fault displays simplify daily inspection and reduce maintenance time.

Electronic controls provide another practical advantage. Remote control operation allows the operator to position concrete accurately while monitoring the end hose. Anti-overload functions, boom angle monitoring, and outrigger interlocks can improve operating safety when used according to the manufacturer instructions and site procedures.

Operating Benefits and Practical Troubleshooting

A pump truck can reduce manual handling, shorten concrete placement time, and improve access to areas that are difficult for transit mixers or wheelbarrows. Fast placement is especially valuable when concrete workability must be maintained across a large pour. Accurate boom positioning can also reduce rehandling and help crews place concrete closer to its final location.

Before pumping, confirm that outriggers are fully deployed on firm support, the boom has adequate clearance from structures and power lines, and the pipeline is securely clamped. Use a suitable priming mortar or approved lubricant according to the concrete supplier and equipment manufacturer requirements. Concrete mix design must be compatible with the pipeline diameter, pumping distance, and aggregate size.

ProblemLikely CausePractical Action
Low pumping outputRestricted line, poor priming, worn pumping parts, or unsuitable mix.Check pipeline bends and clamps, verify mix consistency, inspect wear components.
Pipeline blockageSegregated concrete, long delay, oversized aggregate, or insufficient lubrication.Stop pumping safely, relieve pressure, follow the manufacturer blockage-clearing procedure.
Boom movement is slow or jerkyLow hydraulic oil, clogged filter, incorrect oil temperature, or control issue.Inspect oil level, filter condition, cooler operation, and error indicators.
Hydraulic oil overheatingDirty cooler, sustained high load, low oil level, or cooling fan fault.Clean the cooler, check fan and oil level, reduce abnormal loading.
Concrete leakage at hopper or valve areaWorn seals, loose fasteners, or damaged wear parts.Shut down safely, inspect seals and fastening points, replace worn parts.

Daily care has a direct effect on uptime. Wash the hopper and delivery system after each shift, inspect the wear plate and cutting ring at scheduled intervals, grease boom pins as specified, check hydraulic oil condition, and examine delivery pipes for thinning. Never open a pressurized pipeline or attempt to clear a blockage without following the equipment manufacturer's safety procedure.

When comparing machines, request documented specifications for maximum theoretical output, maximum concrete pressure, boom reach, delivery cylinder size, hopper capacity, and recommended aggregate size. A well-matched pump truck with verified material quality and dependable maintenance support can provide stronger jobsite productivity than a machine selected only for its initial cost.

Original source: https://www.concrete-pump-cn.com/a/concrete-pump-truck-price.html

Self Loading Mobile Concrete Mixer

  Self loading mobile concrete mixers combine loading, batching, mixing, travel, and discharge functions in one machine. That integration re...